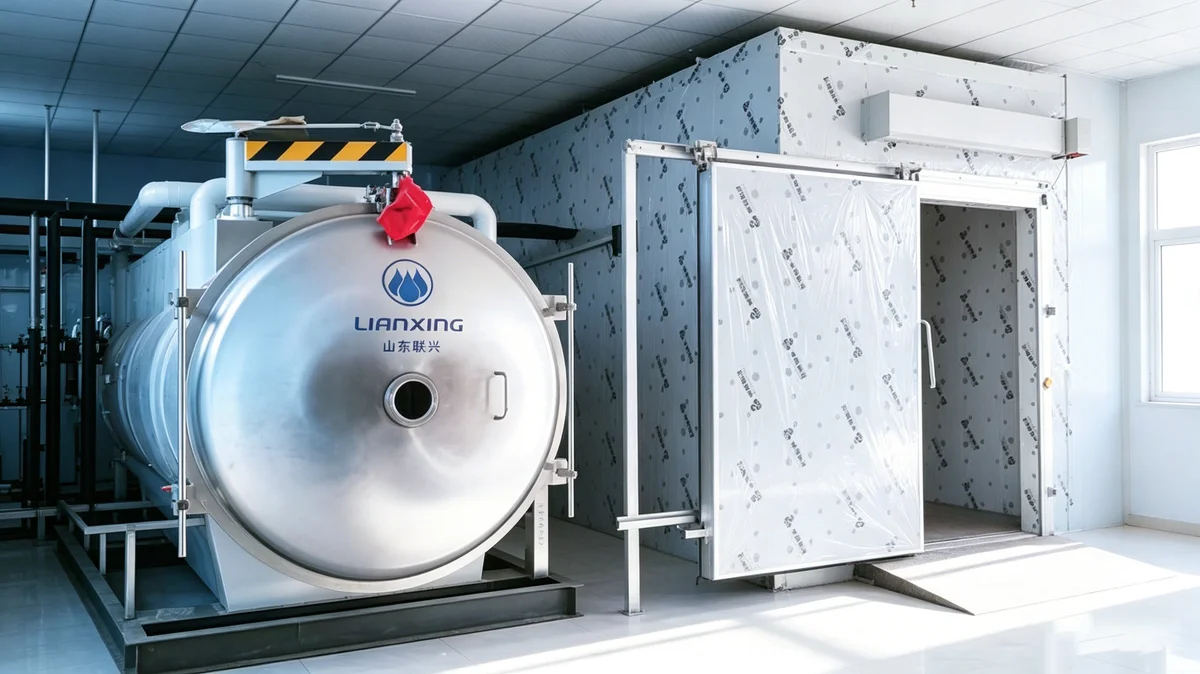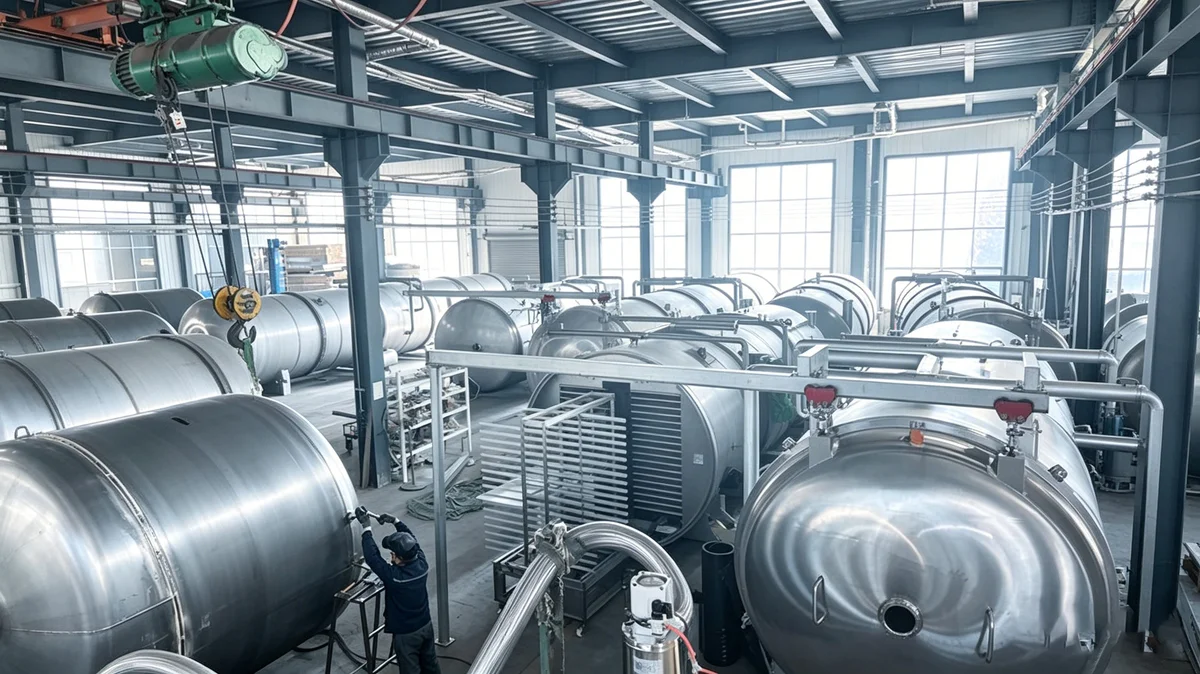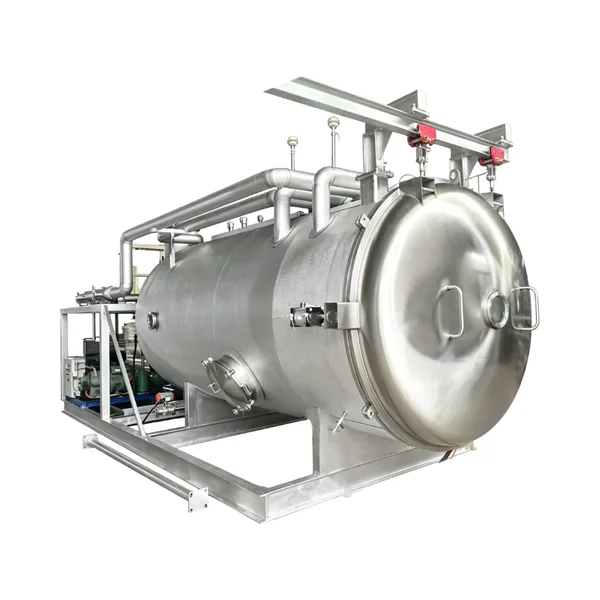
LXFD-NH120|120㎡ Industrial-Grade Steam-Heated Vacuum Freeze Dryer
Large-scale industrial continuous production / Bulk delivery for large orders / Parallel scheduling of multiple product categories / For factories already equipped with steam boilers
LXFD-NH120|120㎡ Industrial-Grade Steam-Heated Vacuum Freeze Dryer (Freeze Dryer)
English LXFD-NH120|120㎡ Industrial Steam-Heated Vacuum Freeze Dryer
Positioning tags: Large-scale industrial continuous production / Bulk delivery for large orders / Parallel scheduling of multiple product categories / For factories already equipped with steam boilers
Suitable materials / application scenarios:
- Health and high-activity nutrition products: probiotics, freeze-dried powder, raw materials for medical food
- Premium pet food and raw meat (BARF): freeze-dried meat sources such as chicken breast, lean beef, and offal
- Fruit and vegetable instant ingredients: strawberry, apple slices, blueberry, banana, mango, durian, broccoli, sweet corn, tomato slices, matsutake
- Seafood and high-protein ingredients: cod fillets, yellow croaker, oysters, shrimp
Applications: continuous mass production in large food factories, brand owners building their own large-scale freeze-drying lines, large OEM factories taking on full-container export orders, factories already equipped with steam boilers
Overview of key parameters:
- Effective drying area: 120 ㎡ (2× the chamber capacity of the NH60)
- Loading capacity per batch: 900 ~ 1500 kg (based on fruits/vegetables and meat materials)
- Heating method: steam heating
- Installed power: 246 kW | Steam consumption: 320 kg/h
- Trays: 272 trays / 4 carts (710×630×35 mm, common to the entire series)
- Dimensions: 12800 × 3100 × 4000 mm | Total weight: approx. 18 T
Core system indicators: ultimate vacuum 5~10 Pa; working vacuum 10~80 Pa (precisely controlled by a thin-film capacitive gauge, 30 Pa ± 2 Pa during the sublimation stage); shelf temperature -40℃ ~ +40℃; temperature uniformity ±1℃; dehydration rate 95%~99%; SUS304 food-grade stainless steel chamber.
Features:
1. 120㎡ large chamber + 4 carts with 272 trays, 900–1500 kg per batch enabling continuous production
The loading capacity per batch is twice that of the NH60; the 4-cart configuration supports loading and unloading by cart and rotational scheduling, with one cart discharging while another loads, minimizing equipment idle time. Together with the NH240, it can form a stepped capacity matrix, flexibly allocated according to order fluctuations.
2. Permanent-magnet variable frequency + stepped vacuum, 15%–25% overall energy savings
With the same energy-saving architecture, measured with 1 ton of raw material: power consumption per ton of finished product drops from about 2200 kWh to about 1780 kWh (-19.1%); energy consumption in the vacuum pulling stage is reduced by 22%; cooling water consumption per batch drops from 12 m³ to 9.5 m³ (-20.8%). The larger the model, the more pronounced the energy consumption advantage per unit of capacity.
3. Locks in color, freshness, and activity
Freeze-dried fruits and vegetables retain 94.5% of VC (hot-air drying only 18%), with a color difference ΔE ≤ 1.2 (imperceptible to the naked eye); probiotic viability increases from 35% with conventional drying to 96.2%; the protein denaturation rate of pet raw meat is ≤ 2.5%, and rehydration restores the original raw meat texture in ≤ 15 seconds.
4. Fully automatic PLC + process database, high batch-to-batch consistency in mass production
One-touch touchscreen setting of plate temperature and vacuum for each stage—pre-freezing, sublimation, and desorption—with automatic recording of the entire batch's process data throughout the run (auditable for Industry 4.0). The category process curves established with the NH60 (fruit/vegetable/seafood/meat) can be directly transferred to the NH120, eliminating the need to re-explore during scale-up.
Precision mass production and process scale-up The LXFD-NH120 is the mainstay of scaled delivery in the FD series. It scales up the process curves validated on the 60㎡ model proportionally to the chamber capacity, giving factories both capacity headroom when taking on large orders and no compromise on quality and batch consistency.
- Large-scale production of freeze-dried strawberries: following the curves measured with the NH60 (700 kg per batch / 20 h / 12:1 shrinkage ratio, sugar-free), after scale-up to the 120㎡ chamber it can match 900–1500 kg per batch feeding, meeting the continuous delivery rhythm of full-container exports.
- Large-scale production of pet raw meat (chicken breast): -35℃~-40℃ ultra-low-temperature deep freezing + 10–40 Pa sublimation, protein denaturation rate ≤ 2.5%, rehydration restores the original meat texture within 15 seconds, and the per-batch cycle is better than the industry-common 22–24 h—no quality degradation even on large models.